Core Box Cleaning for Binder and Release-Agent Buildup
Published · Updated
Plan core box cleaning around binder deposits, release agents, vents and tooling condition. Define a representative test and documented inspection.
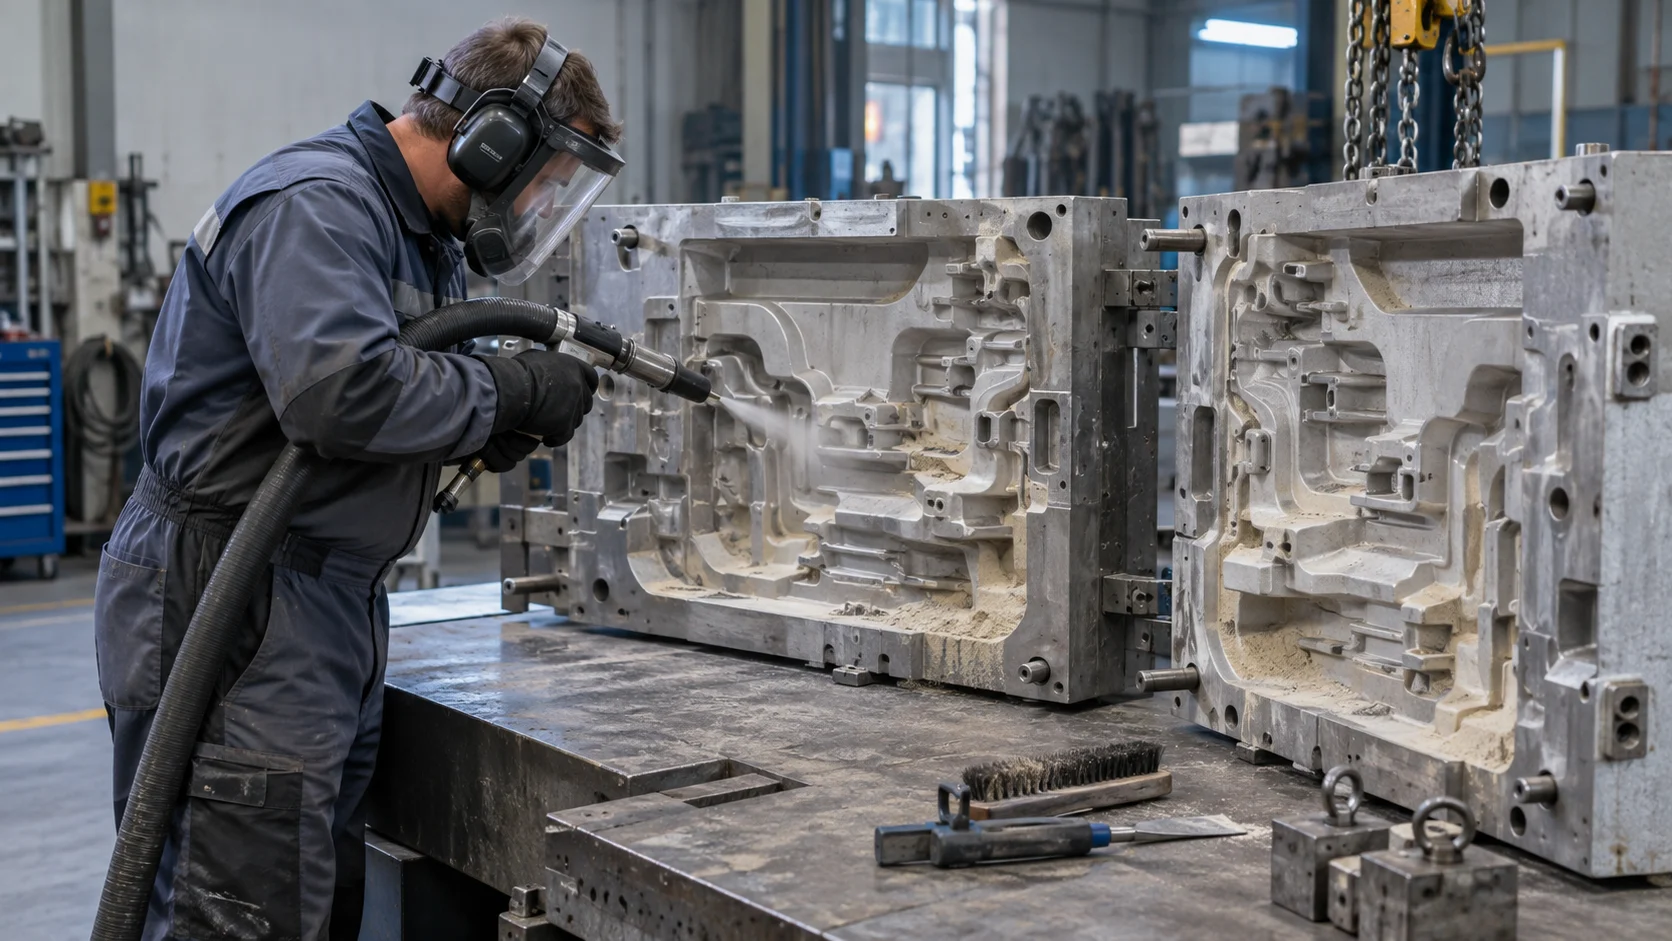
Core box cleaning needs a defined deposit-removal objective and a separate tooling inspection. Identify the binder or release-agent buildup, the affected features and the finish that must remain. Then choose a representative area for evaluation.
Use this suggested framework with your foundry’s tooling and maintenance procedures. The foundry tooling cleaning service explains the wider scope. This guide focuses on the record needed for a core-box review.
Identify the binder and release-agent deposit
Cold Jet lists resin, binder and release-agent removal from core-box tooling among its foundry dry ice cleaning applications. That reference describes possible applications. It does not establish the response of your binder system, coating or tool.
Provide the core process, binder information and release product when available. Include the tool identifier, substrate, coating and repair history. Mark any uncertainty about the deposit instead of treating all buildup as the same material.
Photograph the complete tool and individual deposits. Ask the tooling team to identify which features need inspection after cleaning. Keep observed wear, corrosion and damaged detail on a separate exception list for technical review.
Map the features in the core box cleaning scope
| Area | Record before the test | Review after cleaning |
|---|---|---|
| Cavity surfaces | Deposit location, coating and reference finish | Remaining residue and visible surface condition |
| Vents and screens | Location, access and tooling requirements | Checks specified by the tool owner |
| Parting lines and detail | Existing wear and repair history | Any observed change requiring review |
| Inserts and concealed areas | Removal duties and access restrictions | Areas excluded or needing another method |
Name the person who decides whether a feature is ready for its next step. Keep visual cleaning acceptance separate from dimensional checks, vent assessment and production validation. Record which checks are included in the cleaning visit and which belong to the foundry.
Compare cleaning proposals on equivalent boundaries
Ask each provider to address the same tool sections and deposits. Record whether the proposal assumes the tool stays installed or is removed. Include preparation, handling, transport and reinstatement wherever they apply.
For manual or off-tool methods, ask the tooling owner to identify permitted products and processes. For a dry ice trial, request an assessment of the actual finish and deposit. Avoid selecting a method solely from a published time saving on another foundry’s tool.
Use the quote comparison guide to separate cleaning labor from handling and inspection. Include disposal responsibilities and the expected condition at handback.
Choose a test that represents difficult detail
Select an approved area with the relevant buildup and geometry. Include a detail or edge when it is part of the intended scope and access is suitable. Avoid basing the estimate entirely on a simple flat section.
Agree on the deposit to remove, the surface to retain and the inspection criterion. Record the test location and actual time separately from setup. Afterward, document remaining material and any observed surface change before discussing a larger scope.
Use the test cleaning report to record the decision. Options can include proceeding within tested limits, revising access, retesting another deposit or assessing another method.
Resolve tool access and released material
Ask the owner to specify the condition in which the tool will be handed over. Assign opening, lifting, isolation and other preparation to named personnel. Where work takes place near production, review the boundary with the responsible site team.
Provide available deposit information for the collection plan. Identify adjacent equipment and areas that must remain outside the work zone. Review air supply, ventilation, noise and material handling through the facility assessment.
Use the facility checklist and shutdown planner to collect the access and timing decisions.
Record cleaning and tooling decisions separately
At handback, list completed sections, remaining deposits and inaccessible features. Attach approved photographs and identify the reviewer. Refer dimensional or repair concerns to the tooling team instead of treating deposit removal as a completed repair.
For later visits, keep the binder, release product and operating conditions with the tool record. Reassess the scope when any of those inputs change. Compare the same inspection points before extending an earlier work allowance to new tooling.
Get a core box cleaning quote
Send tool photographs, binder and coating details, location and your proposed work window. Identify the person who approves the inspection criteria. Get a foundry tooling cleaning quote and use the maintenance log to retain the baseline and repeat-visit records.